Guides
Part of Silver sawing and piercing guide: layout, blades, support, turns, and cleanup
How to pierce a clean interior shape in sheet silver
Cut a clean interior opening in sheet silver by drilling in the waste, threading the blade, and rotating the work instead of forcing the saw.
What to take away
- Drill the entry hole in the waste, not on the finished line, so the first stroke has room to settle.
- Keep the blade vertical and turn the sheet into the blade; levering sideways snaps blades and bows the cut.
- Cut on the waste side of the line and watch the tooth line, not the top of the frame.
- Stop and check tension, direction and support when the blade stops cutting; pushing harder bends it.
- File to a measured checkpoint, not to how smooth the edge looks.
This assumes supervised training on the jeweler's saw and the drill. Follow the tool maker's instructions and your studio's controls. Do not drill handheld sheet.
Lay out a test pattern first
Cut one opening that carries a straight run, an outside curve, an inside curve and one corner. Make the webs between openings wider than the finished piece needs, so a small slip still leaves metal.
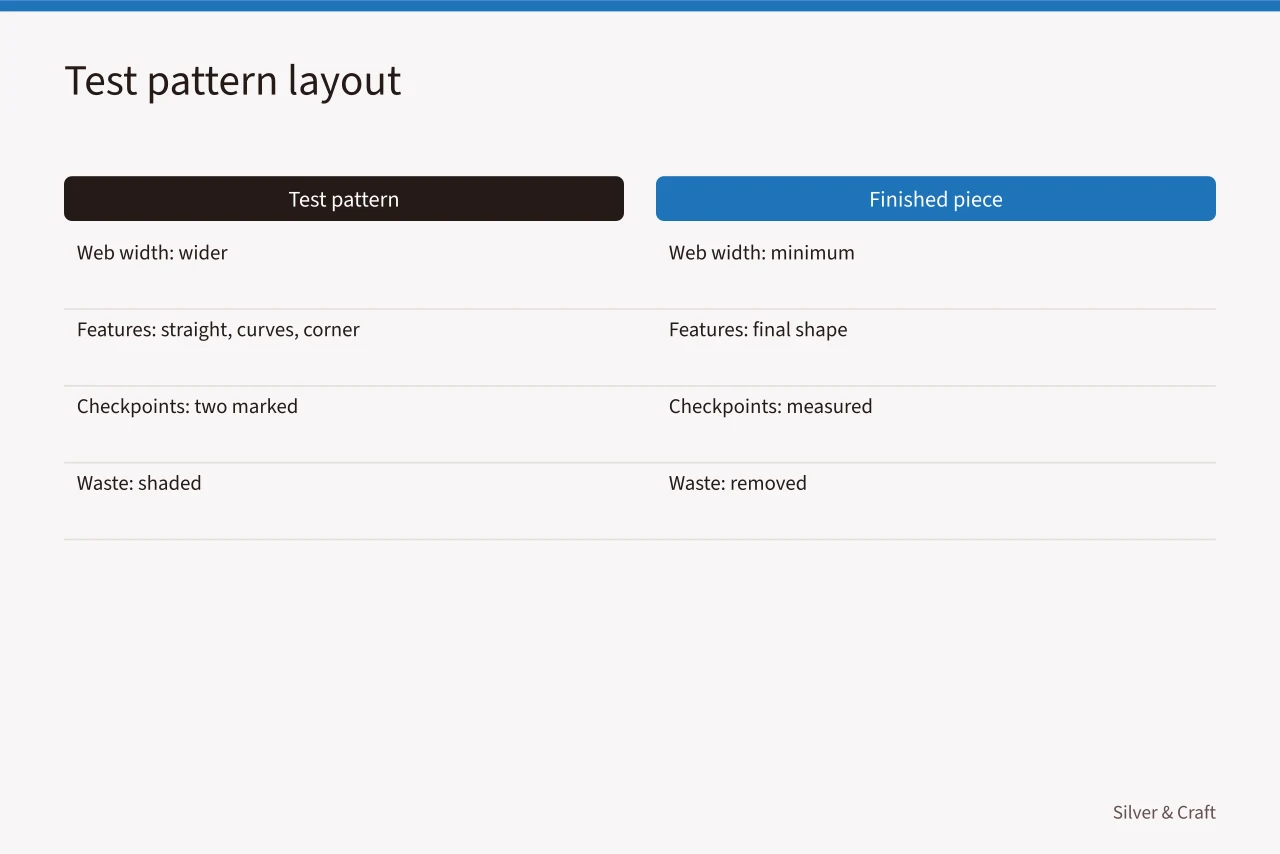
Mark a centerline and two checkpoints you can measure. Shade the waste. Write the alloy, thickness and pattern version on the protective film or a tag tied to the sheet.
Transfer the design
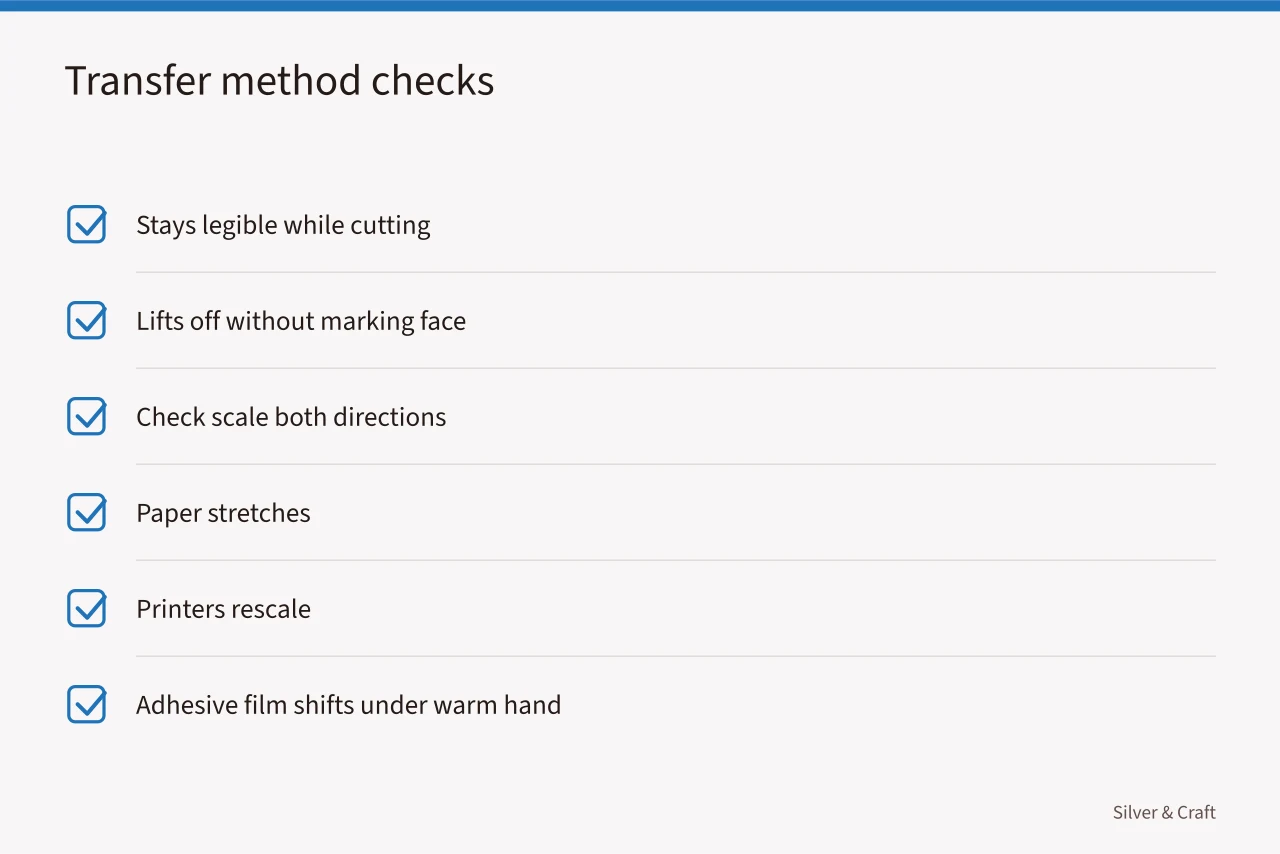
Pick a transfer method that stays legible while you cut and lifts off without marking the face you intend to keep. Check the scale in both directions before you drill. Paper stretches, printers rescale, and adhesive film shifts under a warm hand.
Pierced openwork is a defined metalworking approach, not a decorative label. A University of Wisconsin-Milwaukee summer workshop program lists transferring an image to metal, piercing entry holes, sawing shapes and cleaning them with filing and sanding. Use it for sequence; the dimensions for your opening come from your own drawing.
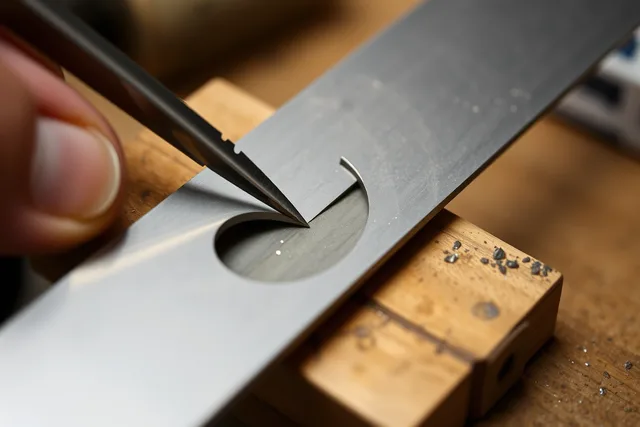
Drill the entry hole
Put the hole in the waste, close enough to the line that the blade reaches it without a long approach. Keep it clear of the finished boundary unless the drawing calls for the drill radius there.
Clamp the sheet or hold it in a vise. Choose a bit rated for the alloy and thickness. Eye protection on, hair and sleeves tied back, and follow the machine's speed, guarding and work-holding instructions. After drilling, break only the burr that would catch the blade. Do not open the hole up by habit.
Thread and tension the saw
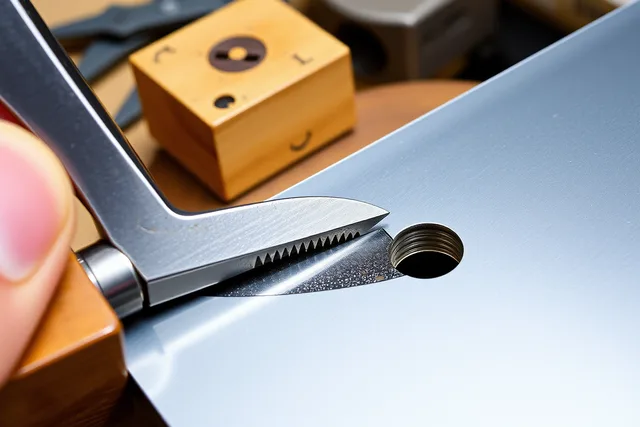
Release one blade end, pass it through the hole, and reclamp it the way the frame specifies. Tension it until it rings at a light pluck. A slack blade cuts a curved kerf in straight stock; an over-tensioned one snaps at the clamp.
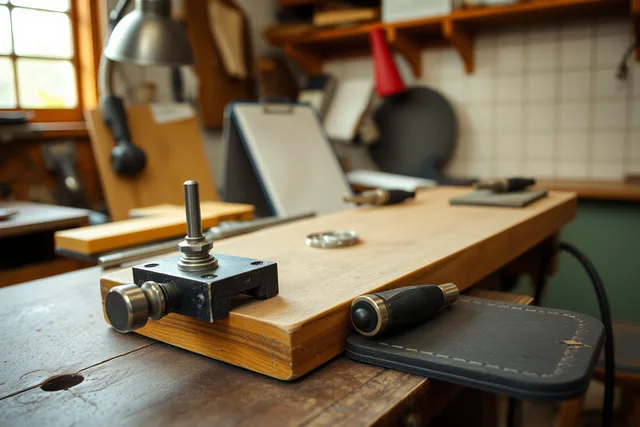
Rest the sheet flat on the bench pin with the opening in view and close to support. Keep your fingers beside the line, never in the downward path of the blade.
Start the cut
Take several short strokes before you steer. Let the teeth cut their own kerf. Once the blade holds a line, settle into a steady vertical rhythm and feed the work into it.
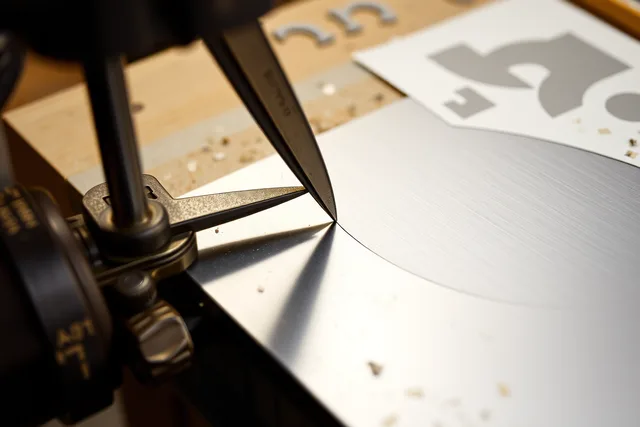
Approach the boundary from the waste side. Watch the tooth line where it meets the metal, not the top of the frame. If the blade stops cutting, stop sawing. Check direction, tension, tooth condition, lubrication and support before you add pressure. Pressure bends blades and bows the wall.
Curves, corners and the close of the cut
On a curve, keep the blade running and rotate the sheet in small increments. The frame stays upright. A tight radius needs smaller rotations and enough clearance behind the blade.
At a corner, decide whether the drawing wants a true point or will take a small radius. You can cut into the corner from two directions, or turn inside a relief filed on the waste side. Never twist a stopped blade.
As the cut closes, support the waste so it cannot drop and trap the blade. Finish the path without prying. Release tension before you lift the work out.
Inspect, then file
Keep the interior waste. It confirms the alloy and gives you a coupon for later trials.
Brush off chips and look at the opening under diffuse light and then raking light. Compare it with the centerline and both checkpoints.
Mark the high spots you can remove. Work with a needle file or escapement file, keeping the safe edge against the face you are protecting. A few strokes, clear the chips, measure again.
Filing to a feel for smoothness erases the reference and oversizes the opening.
Acceptance check
- the boundary sits inside tolerance at both checkpoints
- paired features agree across the centerline
- corners carry the planned radius
- no crack, deep notch, folded burr or thin unsupported web
- finishing allowance still on the walls
- waste and notes keep the stock ID
Common questions
Where should the starter hole go?
In the waste, far enough from the line that the blade can settle before it reaches the boundary. Leave room to thread the blade and take a first stroke without crowding the finished edge.
Why does the blade wander on a straight line?
Usually support, tension or side pressure. Check that the sheet sits flat on the pin, the blade rings when plucked, and your fingers are guiding the work rather than steering the frame. A bent or dull blade will also drift.
Should I file before checking symmetry?
No. Measure first. Filing removes the very edge you would measure against, and an opening only grows. Mark the high spots, take a few strokes, then recheck.
Can I practice on unknown sheet?
Use documented stock. An unmarked alloy behaves differently under the saw and the torch, and you lose the coupon that would tell you what you just cut.